01Semiconductor equipment
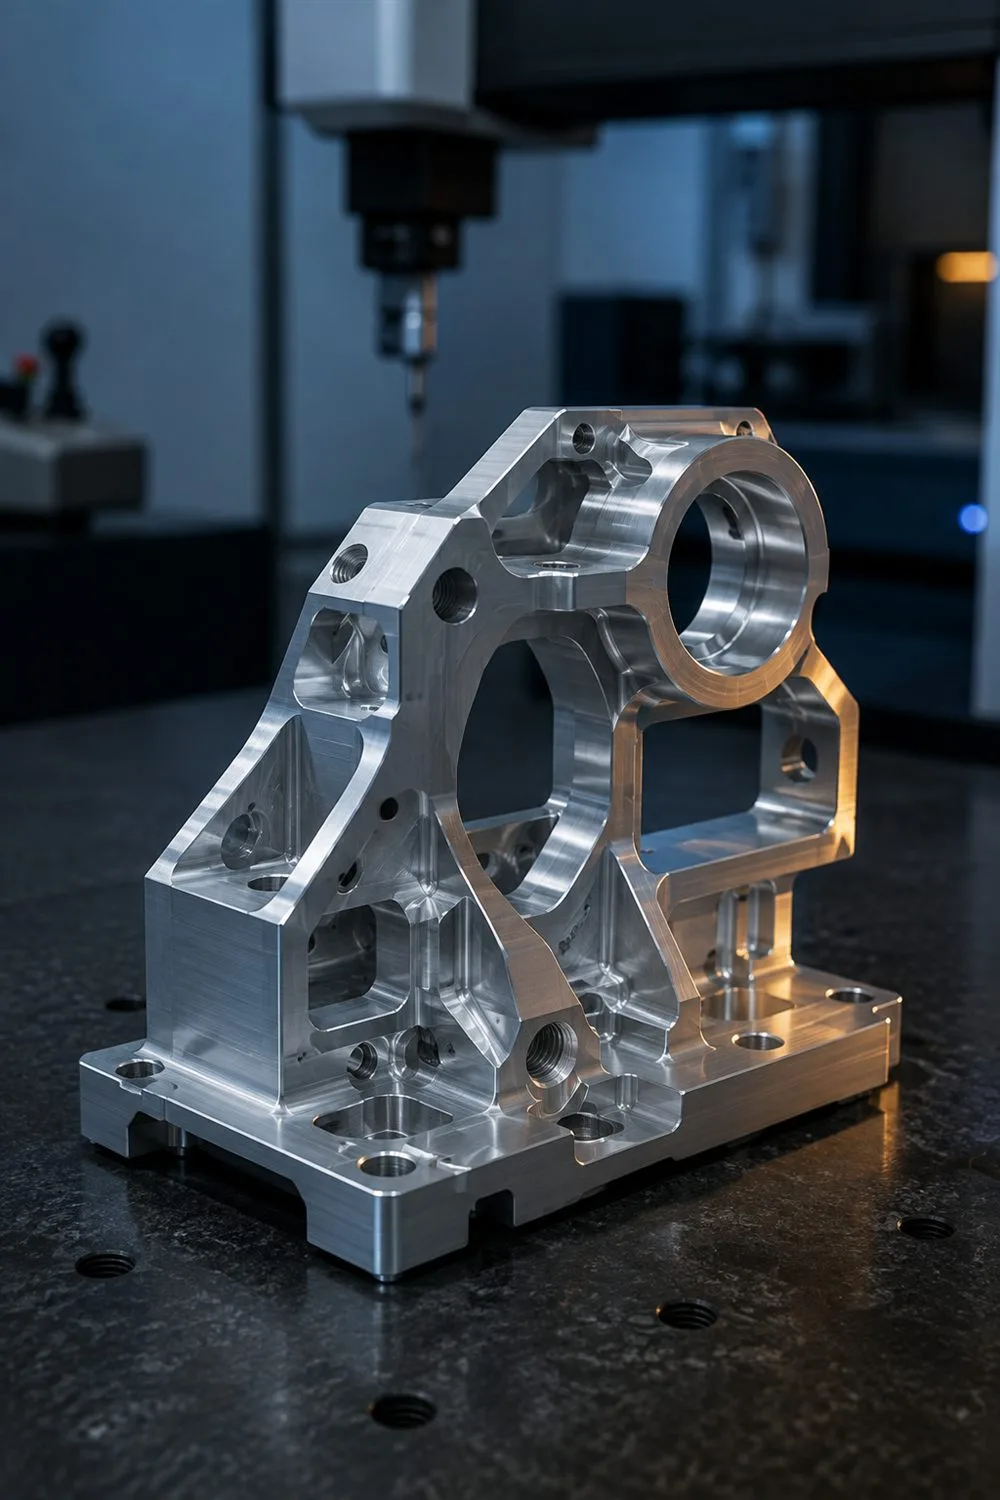
Aluminum locating fixture
Holes at multiple angles are finished in one setup, avoiding position error from re-clamping.
7075-T6±0.008 mm600 pcs / month
Route: Zone A → C → D → E
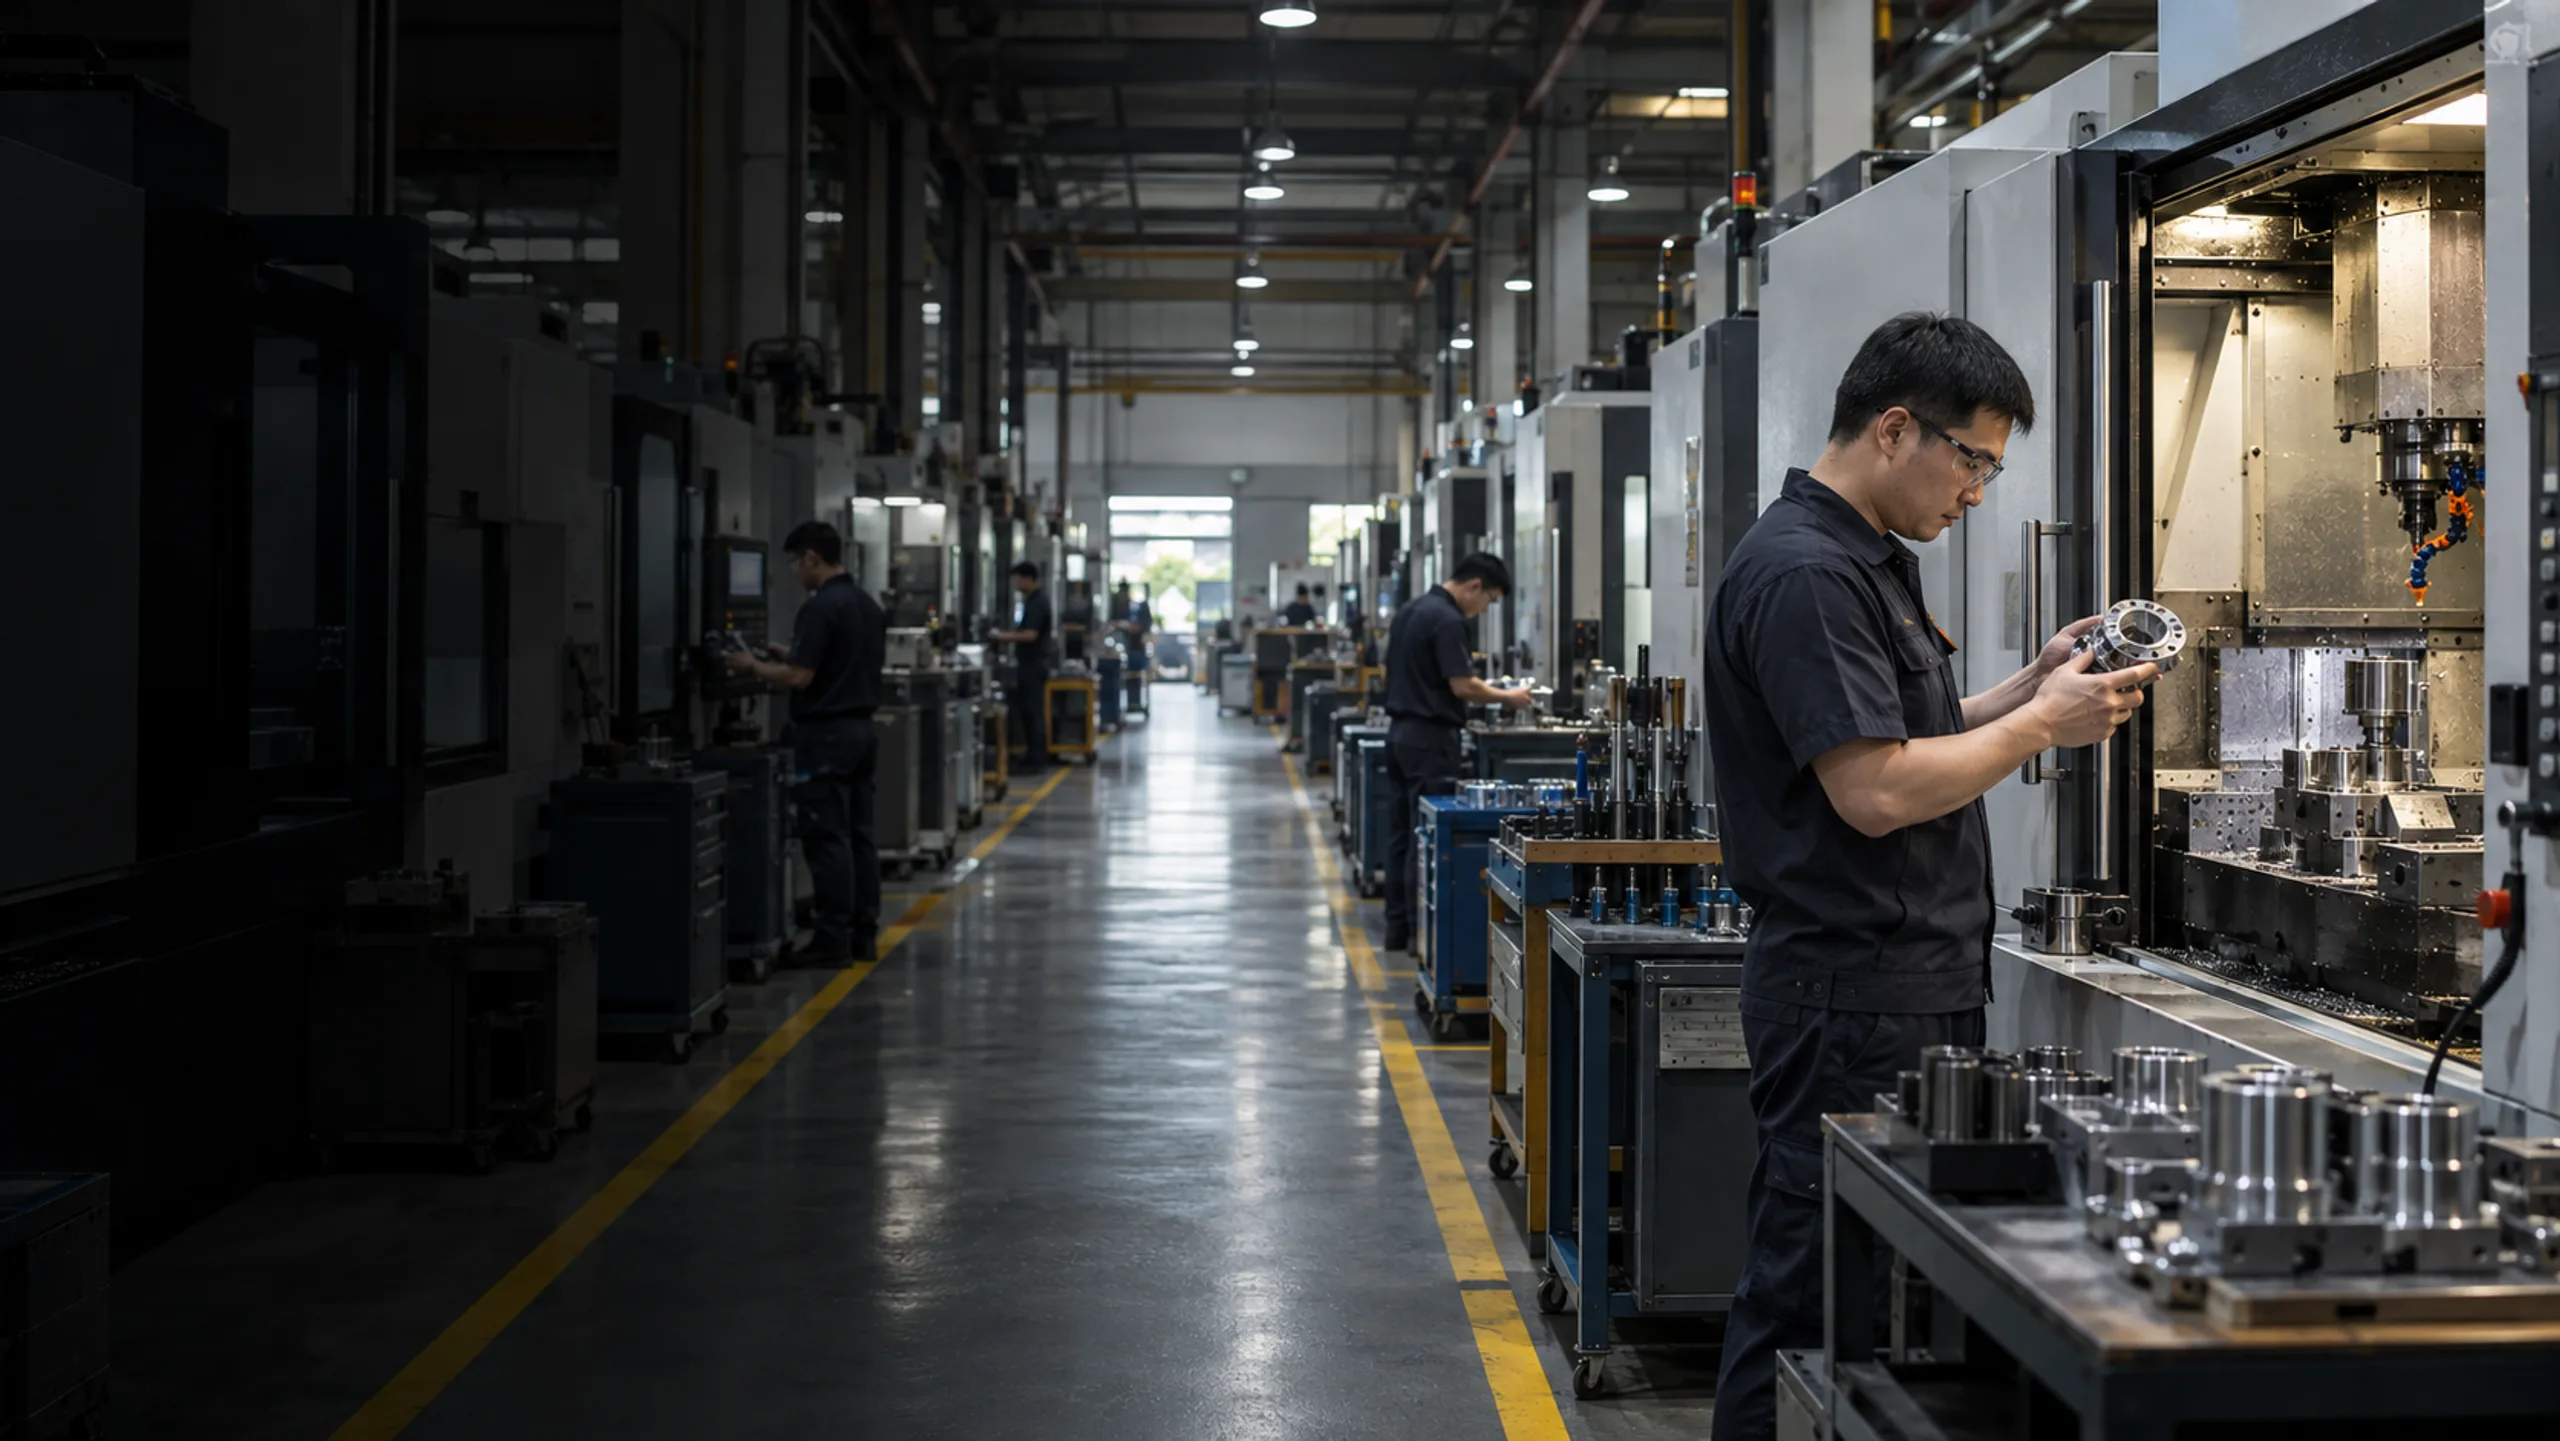
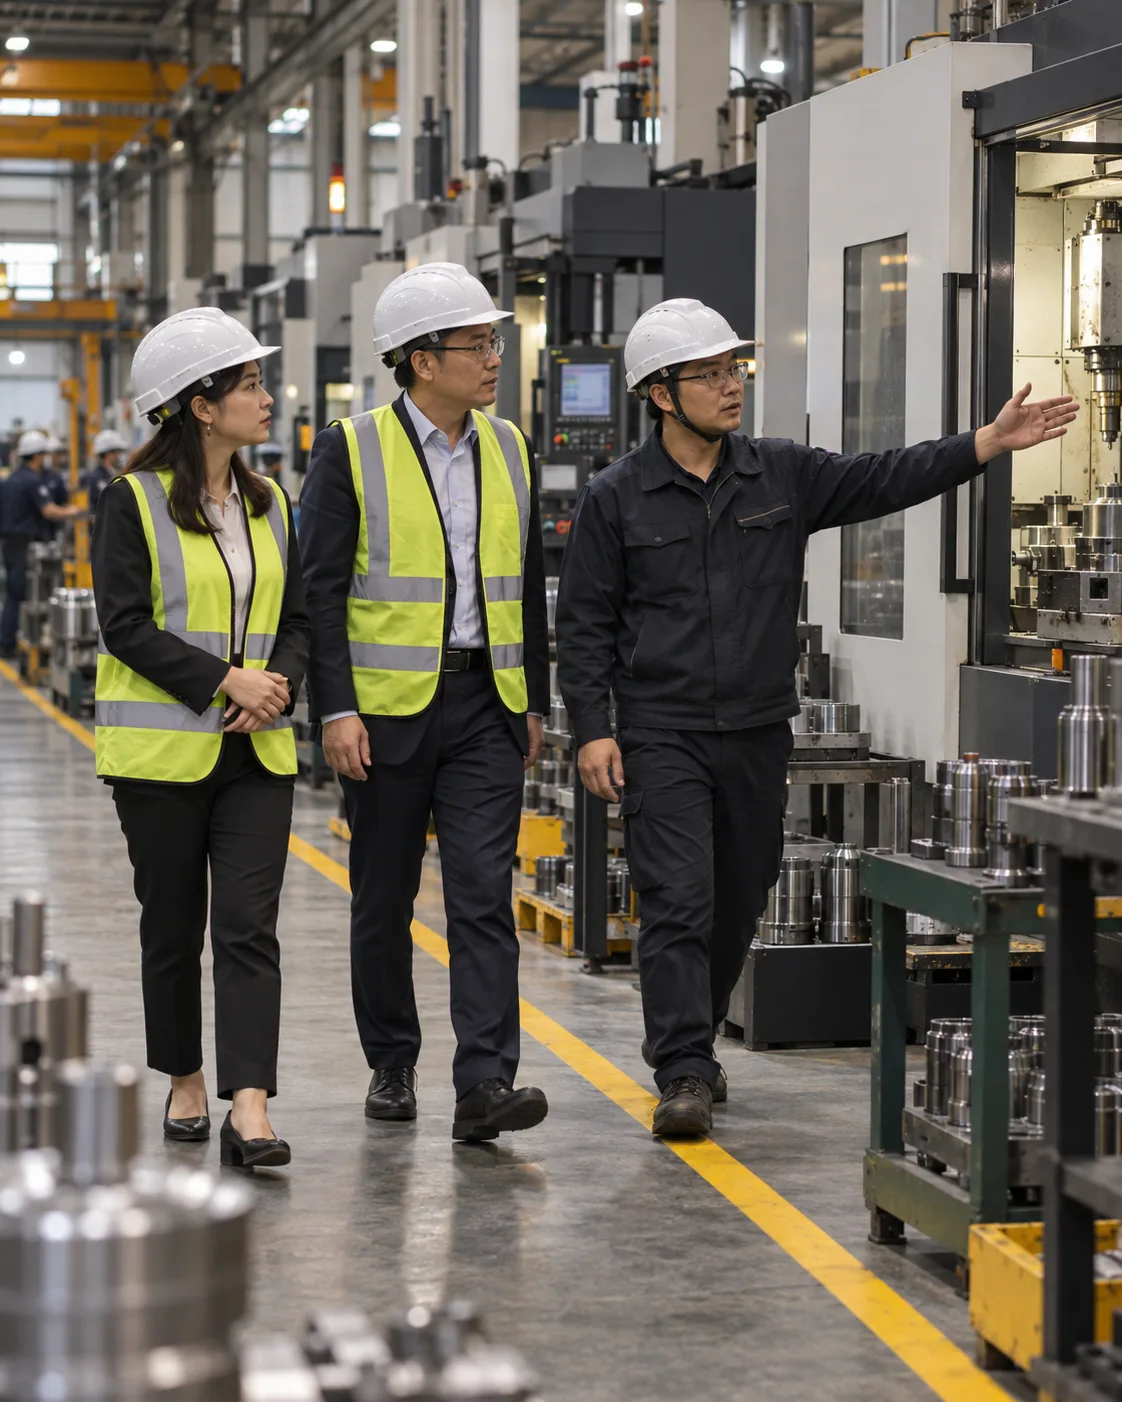
JUCHENG runs two buildings and 42 machines in Taichung, taking parts from prototype to production on one site. Buyers and quality teams can walk the plant here first, then book a time to see it in person.
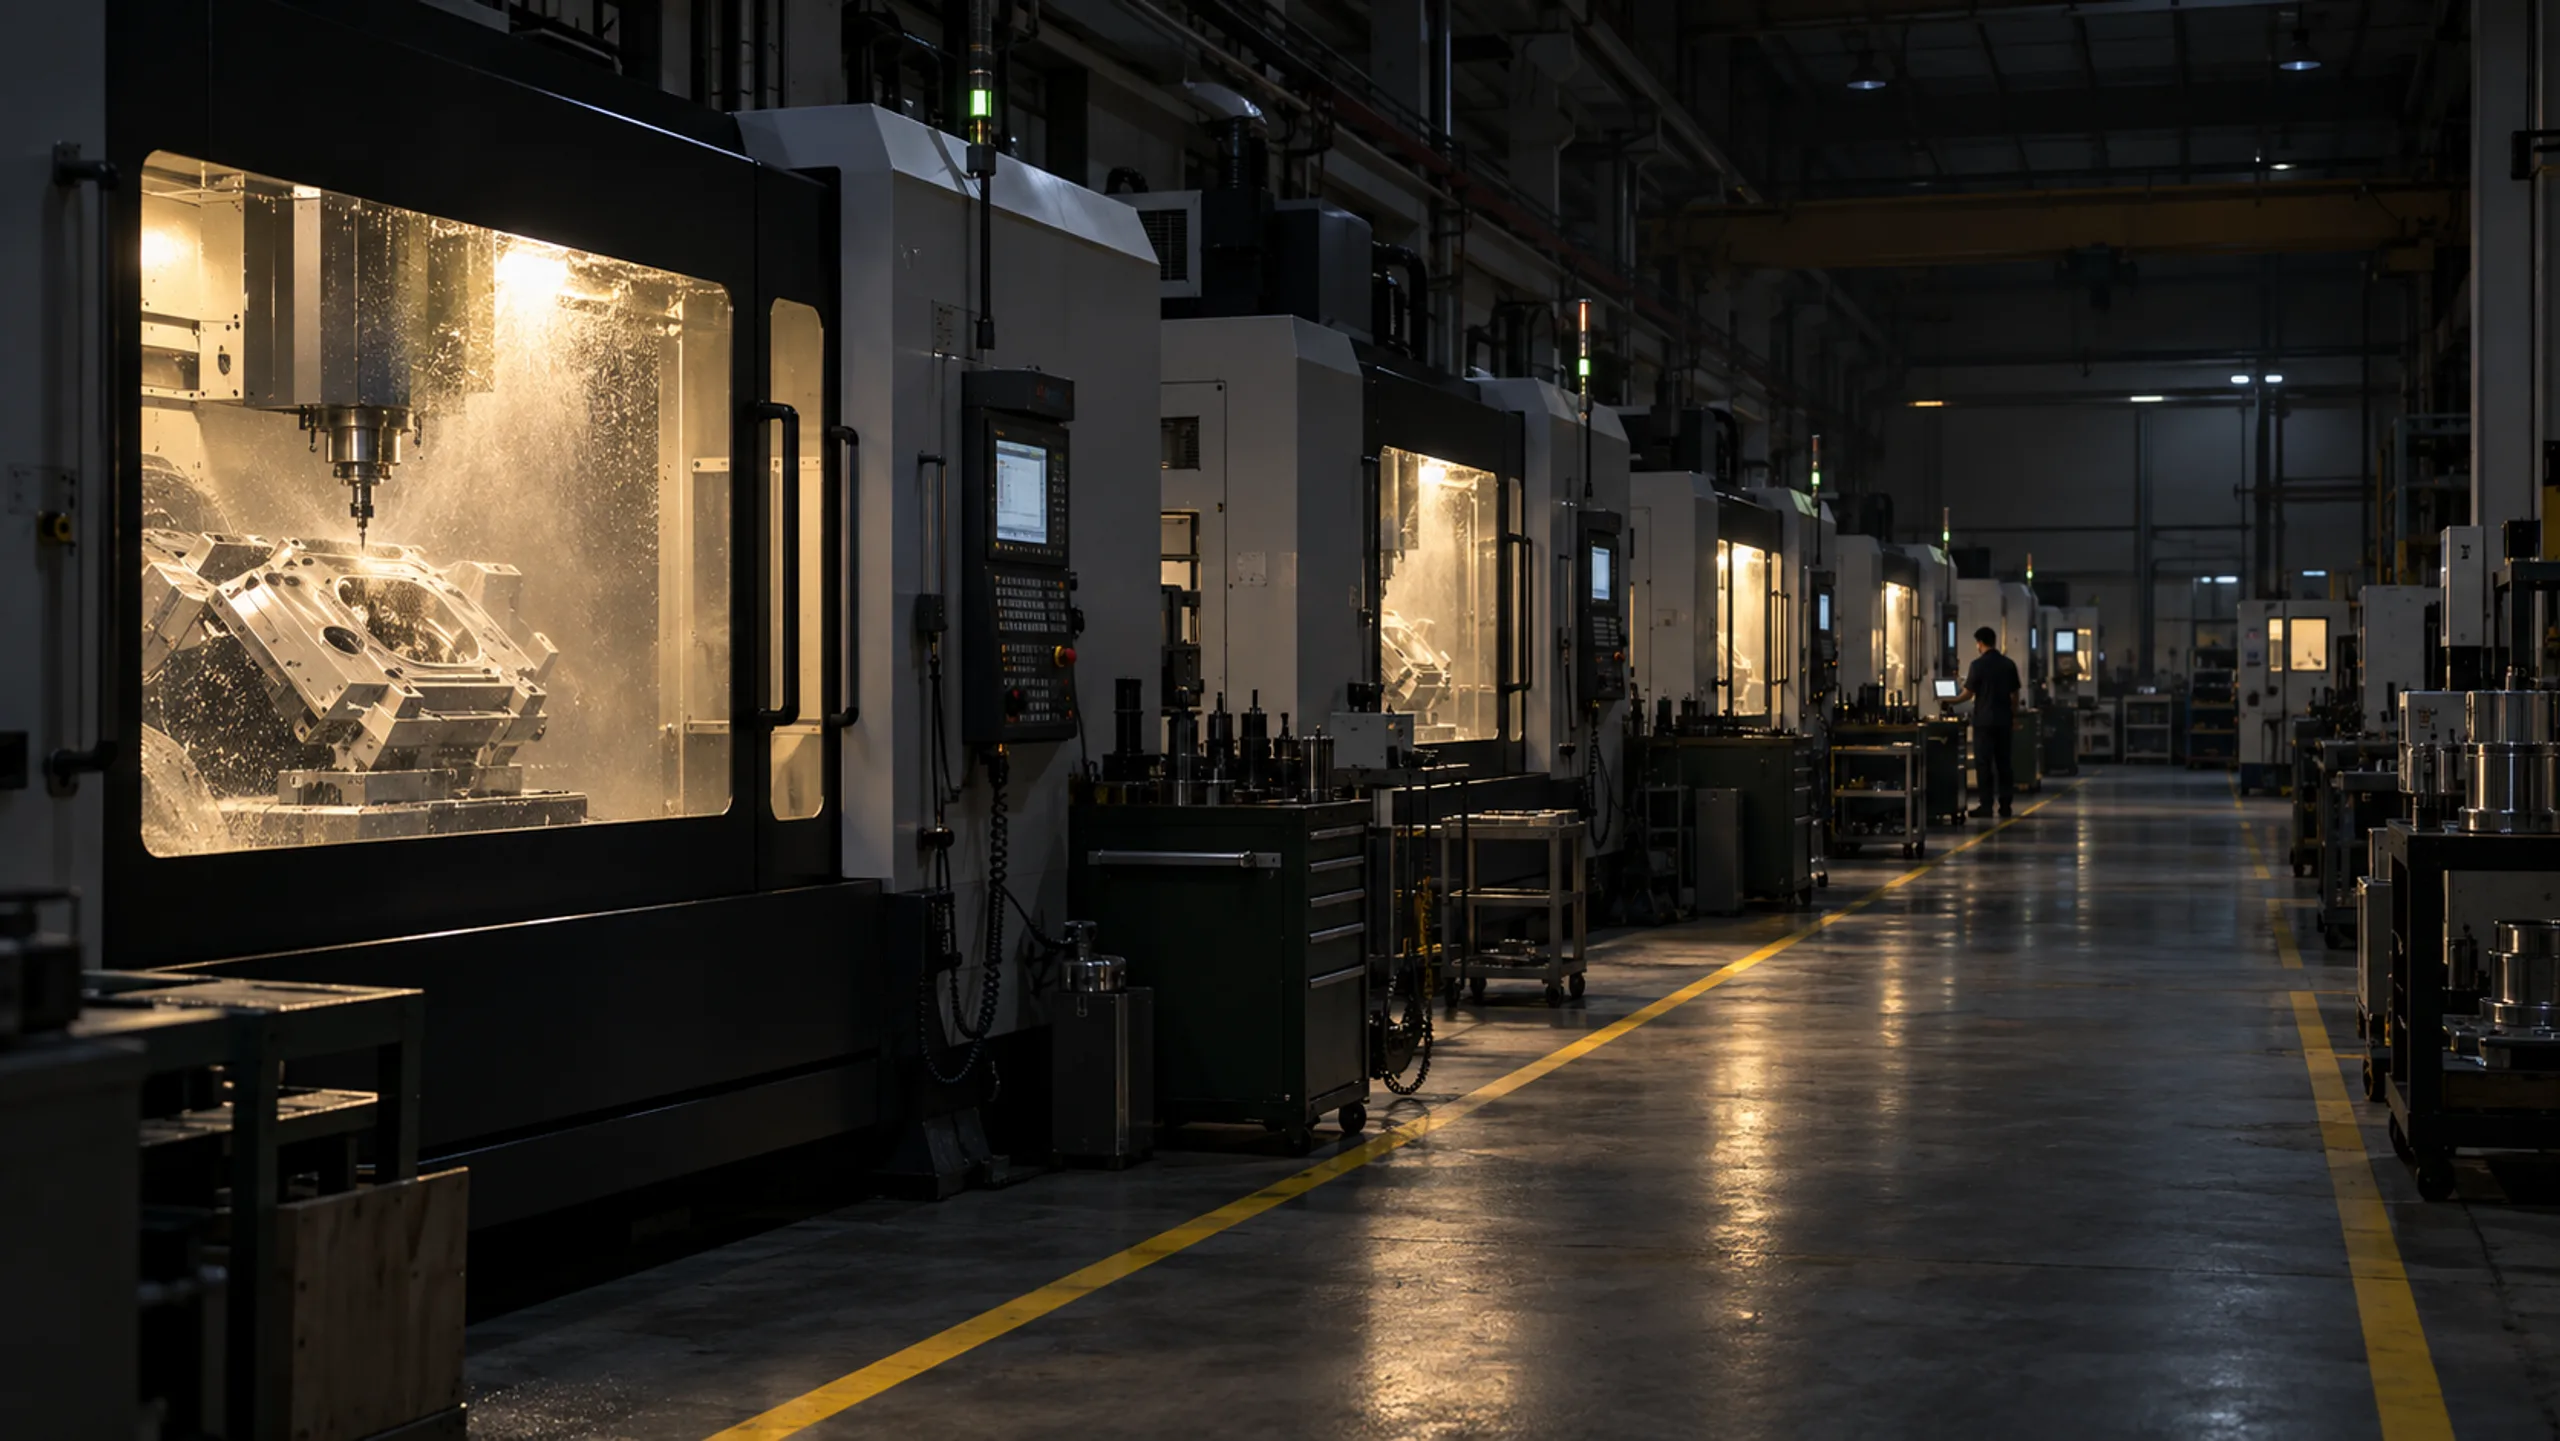
The main lights are off.
The 5-axis machines keep running.
Click a zone on the plan to see what happens there, which machines it holds and who runs them. The yellow dashed line is the route a part takes through the plant.
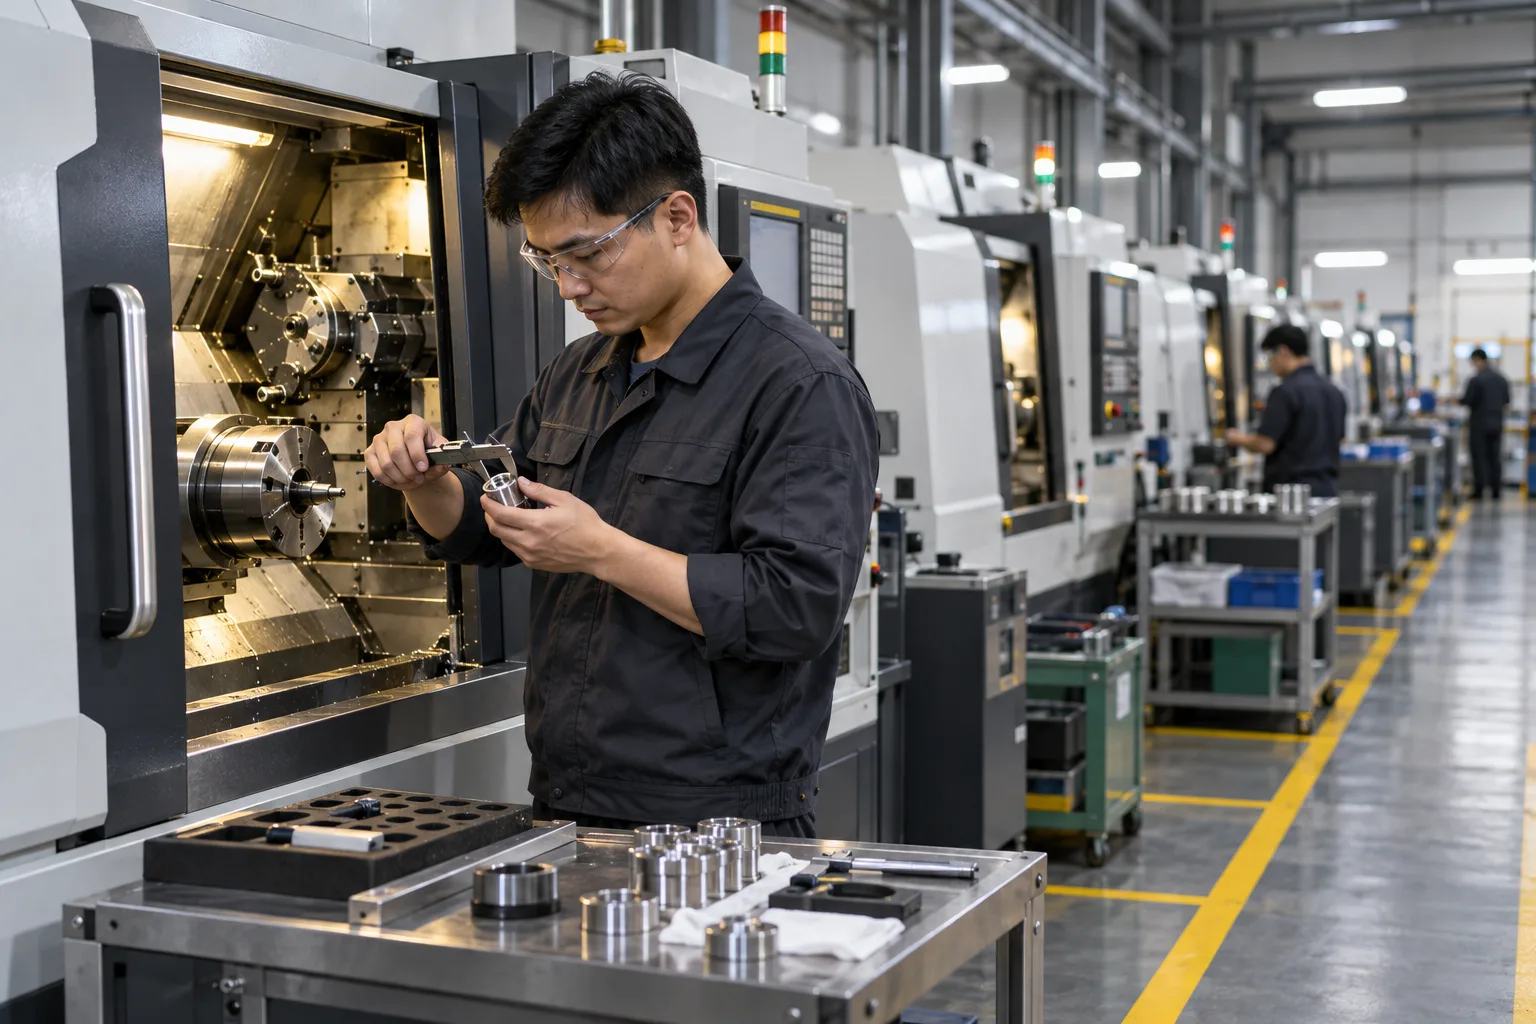 Stop 2 of 5
Bar stock is turned to outside diameter, bore and datum faces here. Each machine keeps its first article and gauges beside it, and both are handed over with the first-article record at shift change.
JUCHENG outsources no process steps. From bar stock to sealed carton, every part stays inside this plant.
Two shifts: day shift runs staffed machines, night shift runs batch work lights-out. Each time slot has a fixed job, so parts never sit waiting on someone's desk.
--:--The shop floor runs on this schedule.
Night shift hands its run logs and any issues to day shift at the machine.
Zones B, CThe first part of every new order goes to metrology. The batch is released only after it passes.
Zone DEvery two hours, quality spot-checks key dimensions and logs them on the work order.
Zones B, CAfternoons are reserved for CMM inspection, with reports filed by lot number.
Zone DToday's shipments are packed in divided cartons, lot-labeled and sent with their reports.
Zone EBatch parts run on bar feeders while two staff on duty patrol machines and change tools.
Zones B, CThese are sample part types for this template. Replace them with photos and specs you are cleared to publish.
Holes at multiple angles are finished in one setup, avoiding position error from re-clamping.
Route: Zone A → C → D → E
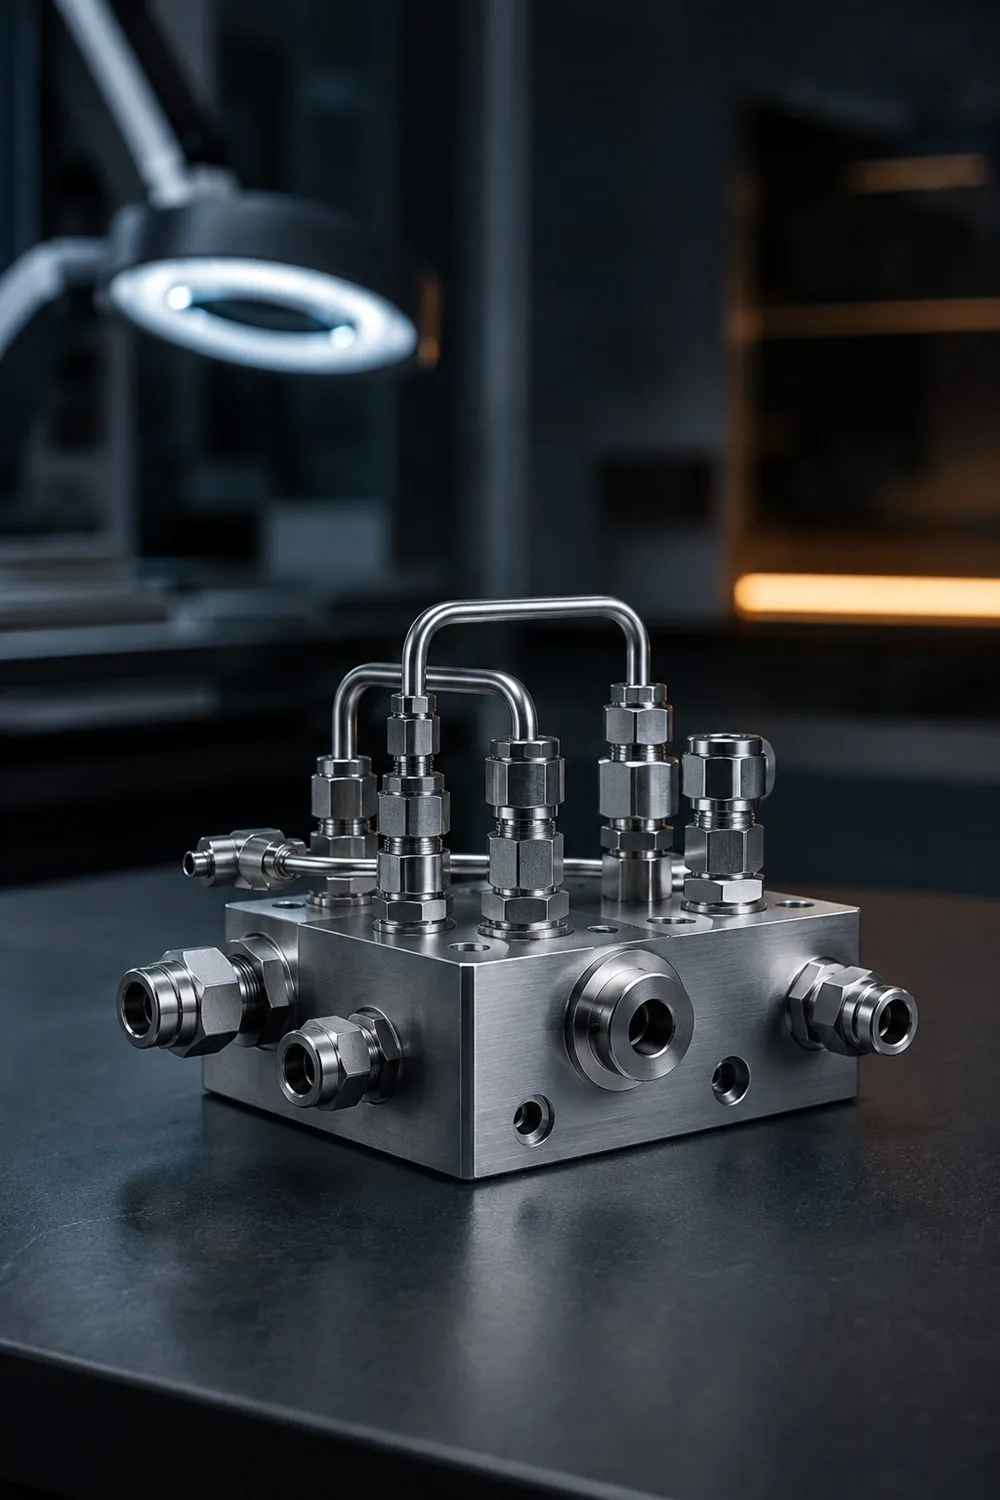
Deep and intersecting bores are leak-tested part by part, with reports shipped alongside.
Route: Zone A → B → C → D → E
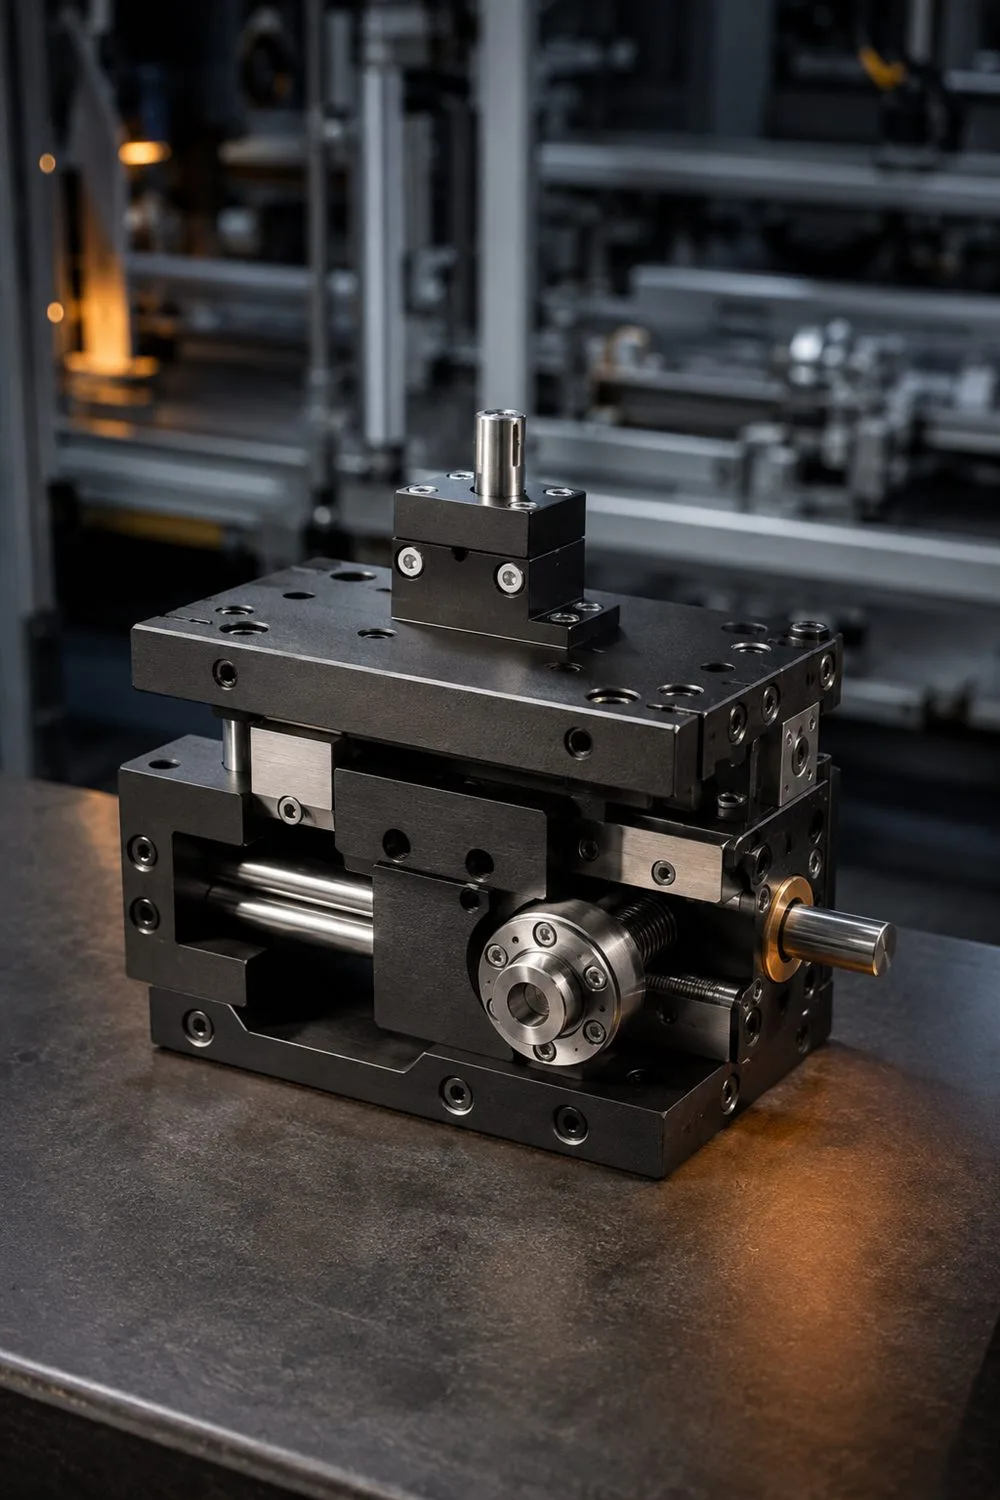
Reworked datums and fewer parts cut assembly time and improve locating repeatability after changeover.
Route: Zone A → B → C → D → E
Every document traces to a lot number. When your quality team needs to trace a part, the carton label leads straight to the machine and shift that made it.
Chemistry and mechanical properties from the mill, checked against the heat number on receipt.
Full-dimension inspection of the first part of a new order. Production starts only after it passes.
Sampled inspection of the critical dimensions on your drawing, with measured values and tolerances.
Appearance, quantity and packing checks, matched against the lot label on each carton.